
Aluminum Strip for Transformer
Transformer manufacturers and electrical fabricators frequently ask practical questions about aluminum strip for transformer windings before placing a production order. Recent discussions across Google searches, Quora-style forums, and industry communities focus less on basic material definitions and more on electrical performance, dimensional control, insulation compatibility, and welding behavior.
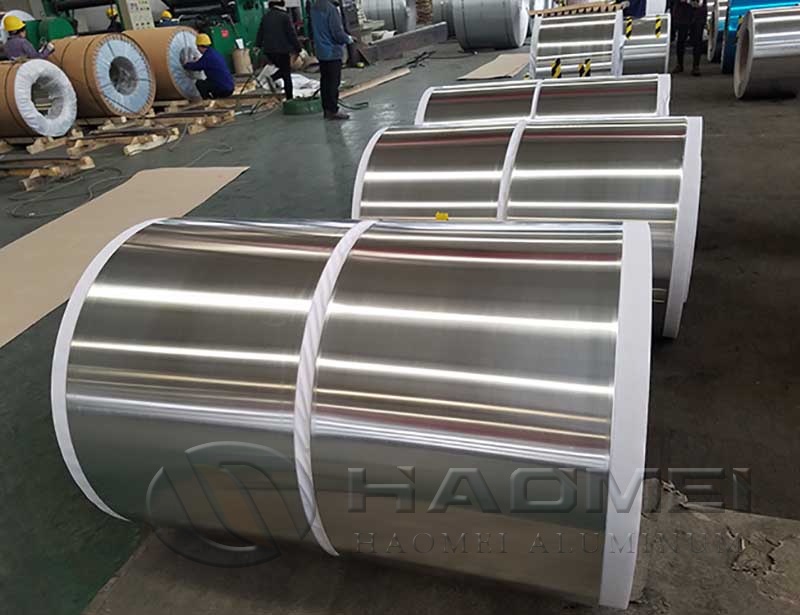
1. Which alloy is best for aluminum strip for transformer winding, 1060 or 1070?
For most transformer windings, 1060 and 1070 are preferred because they are commercially pure aluminum grades with high electrical conductivity, soft forming behavior, and stable performance during winding. The practical difference is that 1070 aluminum strip generally has a slightly higher aluminum content and can provide marginally better conductivity, while 1060 aluminum strip is widely available and often more economical for standard distribution-transformer applications.
The grade should not be selected by conductivity alone. A winding material must also bend consistently around the mandrel without edge cracking, remain flat during tensioning, and accept insulation paper or enamel without surface defects. When the design has a narrow bending radius or a high number of turns, a soft temper such as O temper is usually safer than a harder temper.
| Material option | Typical use | Main advantage | Point to confirm |
|---|---|---|---|
| 1060 aluminum | Distribution transformers, general electrical winding | Good conductivity and broad availability | Actual conductivity requirement |
| 1070 aluminum | Higher-efficiency windings, demanding electrical designs | Higher purity and conductivity | Cost versus loss reduction |
| O temper | Tight-radius winding | Excellent ductility | Dimensional tolerance after slitting |
| H14 or H16 temper | Certain rigid bus applications | Improved stiffness | Suitability for repeated bending |
For applications requiring stable winding performance, specify both alloy and temper on the purchase document. Saying only "pure aluminum" leaves too much room for variation in hardness and processing quality. Manufacturers sourcing Aluminum Strips for electrical use should also request the conductivity value, thickness tolerance, width tolerance, and burr-control requirement.
2. How do I calculate the correct width and thickness for a transformer aluminum winding?
The conductor cross-sectional area is the starting point. In simplified form, the area equals width multiplied by thickness. The required area depends on transformer current, allowable current density, temperature rise, cooling method, and winding arrangement. Increasing width can reduce resistance while keeping the winding relatively thin, but the available window space and insulation build must be considered.
For example, a conductor measuring 20 mm wide by 1.0 mm thick has a cross-sectional area of 20 mm². If a design needs more current capacity, an engineer may increase thickness, width, or both. However, wider material can be harder to wind evenly if the winding machine, insulation layers, and bobbin geometry are not matched.
A useful purchasing practice is to distinguish nominal dimensions from permitted variation. A 1.00 mm thickness with a loose tolerance may cause resistance differences from one lot to another. It may also change the final winding diameter and interfere with insulation spacing. For transformer work, dimensional consistency is often as important as the nominal size.

3. Does aluminum strip need edge deburring for transformer winding?
Yes. Edge condition is one of the most important but often overlooked quality details. Slitting can leave burrs, sharp feathered edges, or slight edge waves. These defects may damage kraft paper, polyester film, aramid insulation, or enamel coatings during winding. A tiny burr can become a long-term reliability concern if vibration, thermal cycling, or winding pressure causes it to work through the insulation barrier.
Ask for a slit edge suitable for electrical winding, with controlled burr height and no severe edge cracking. The appropriate limit depends on thickness and insulation system, but the material should be inspected under magnification when the design uses thin insulation or tightly packed layers.
Surface cleanliness matters as well. Oil residue, dust, oxide particles, and handling marks can reduce insulation adhesion or create winding-machine contamination. High-quality transformer material normally has a clean, uniform surface rather than a decorative finish. If a project requires paper-covered conductor, confirm whether the aluminum will be supplied bare for in-house wrapping or delivered with an insulation system already applied.
4. Can aluminum winding material be welded or brazed reliably in transformers?
Aluminum can be joined effectively, but the joining method must suit the electrical and mechanical design. TIG welding, ultrasonic welding, resistance welding, cold pressure welding, and certain brazing processes may be used depending on conductor thickness, terminal geometry, and production volume. Each method needs careful surface preparation because aluminum oxide forms naturally and melts at a much higher temperature than the base metal.
For low-resistance joints, contact pressure and clean mating surfaces are critical. A joint that looks acceptable visually may still create unwanted resistance, leading to localized heating under load. Connection areas should be assessed with electrical resistance testing rather than appearance alone.
When specifying Aluminium Strips, discuss the intended joining process with the material supplier. A soft, high-purity grade usually works well for forming and cold welding, but surface condition, thickness, and storage conditions can influence results. Avoid assuming that a method proven for copper conductors will produce identical results with aluminum.
5. What inspection items should I request before accepting transformer aluminum material?
A reliable inspection plan should cover chemistry, electrical properties, dimensions, surface quality, and packaging. A mill test certificate is useful, but physical checks on received material remain important, especially for narrow-width products or tight-tolerance designs.
| Inspection item | Why it matters in transformer winding | Typical receiving check |
|---|---|---|
| Alloy composition | Confirms specified 1060 or 1070 grade | Review mill test certificate |
| Electrical conductivity | Influences conductor resistance and losses | Verify reported percentage IACS or resistivity |
| Thickness | Affects current capacity and winding build | Measure at several positions |
| Width | Determines winding fit and insulation clearance | Measure across multiple locations |
| Burr and edge quality | Protects insulation from cutting damage | Visual check and magnified inspection |
| Flatness and camber | Supports smooth machine winding | Unroll a sample length |
| Surface cleanliness | Helps insulation compatibility and joint quality | Check for oil, scratches, and particles |
| Packaging protection | Prevents dents, moisture exposure, and telescoping | Inspect outer wrap and inner support |
For repeat orders, retain a reference sample from an approved lot. Comparing new deliveries against the approved sample makes it easier to identify shifts in temper, edge quality, color, flatness, or winding behavior before material enters production.
Original source: https://www.hm-alu.com/a/aluminum-strip-for-transformer.html
Tags:aluminum strip for transformer transformer winding aluminum 1060 aluminum strip 1070 aluminum strip